Premium Men's Underwear Manufacturing from the Heart of China's Textile Hub
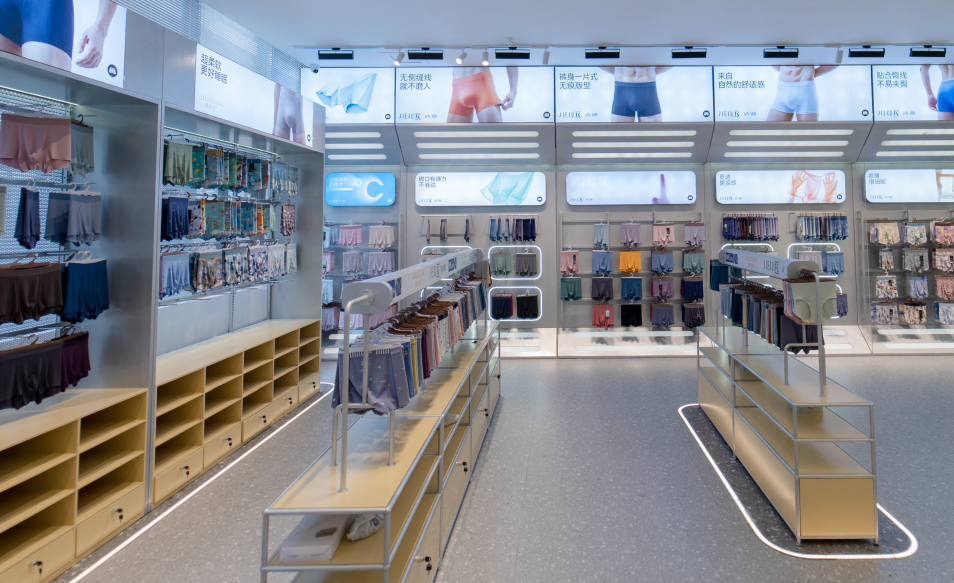
Founded in 2011 in Xiaolan, Zhongshan—celebrated globally as "China's Renowned Underwear Town"—our company has rapidly emerged as a premier OEM/ODM partner for global intimate apparel brands. Spanning a modern 10,000-square-meter facility, we combine regional supply chain advantages with top-tier technical expertise. We are dedicated to delivering exceptional comfort, precise craftsmanship, and reliable scale, empowering clothing labels and fast-growing e-commerce brands with a transparent, retail-ready manufacturing experience.
Established
Facility
Specialists
Annual Output
Modern Infrastructure & High-Volume Scalability
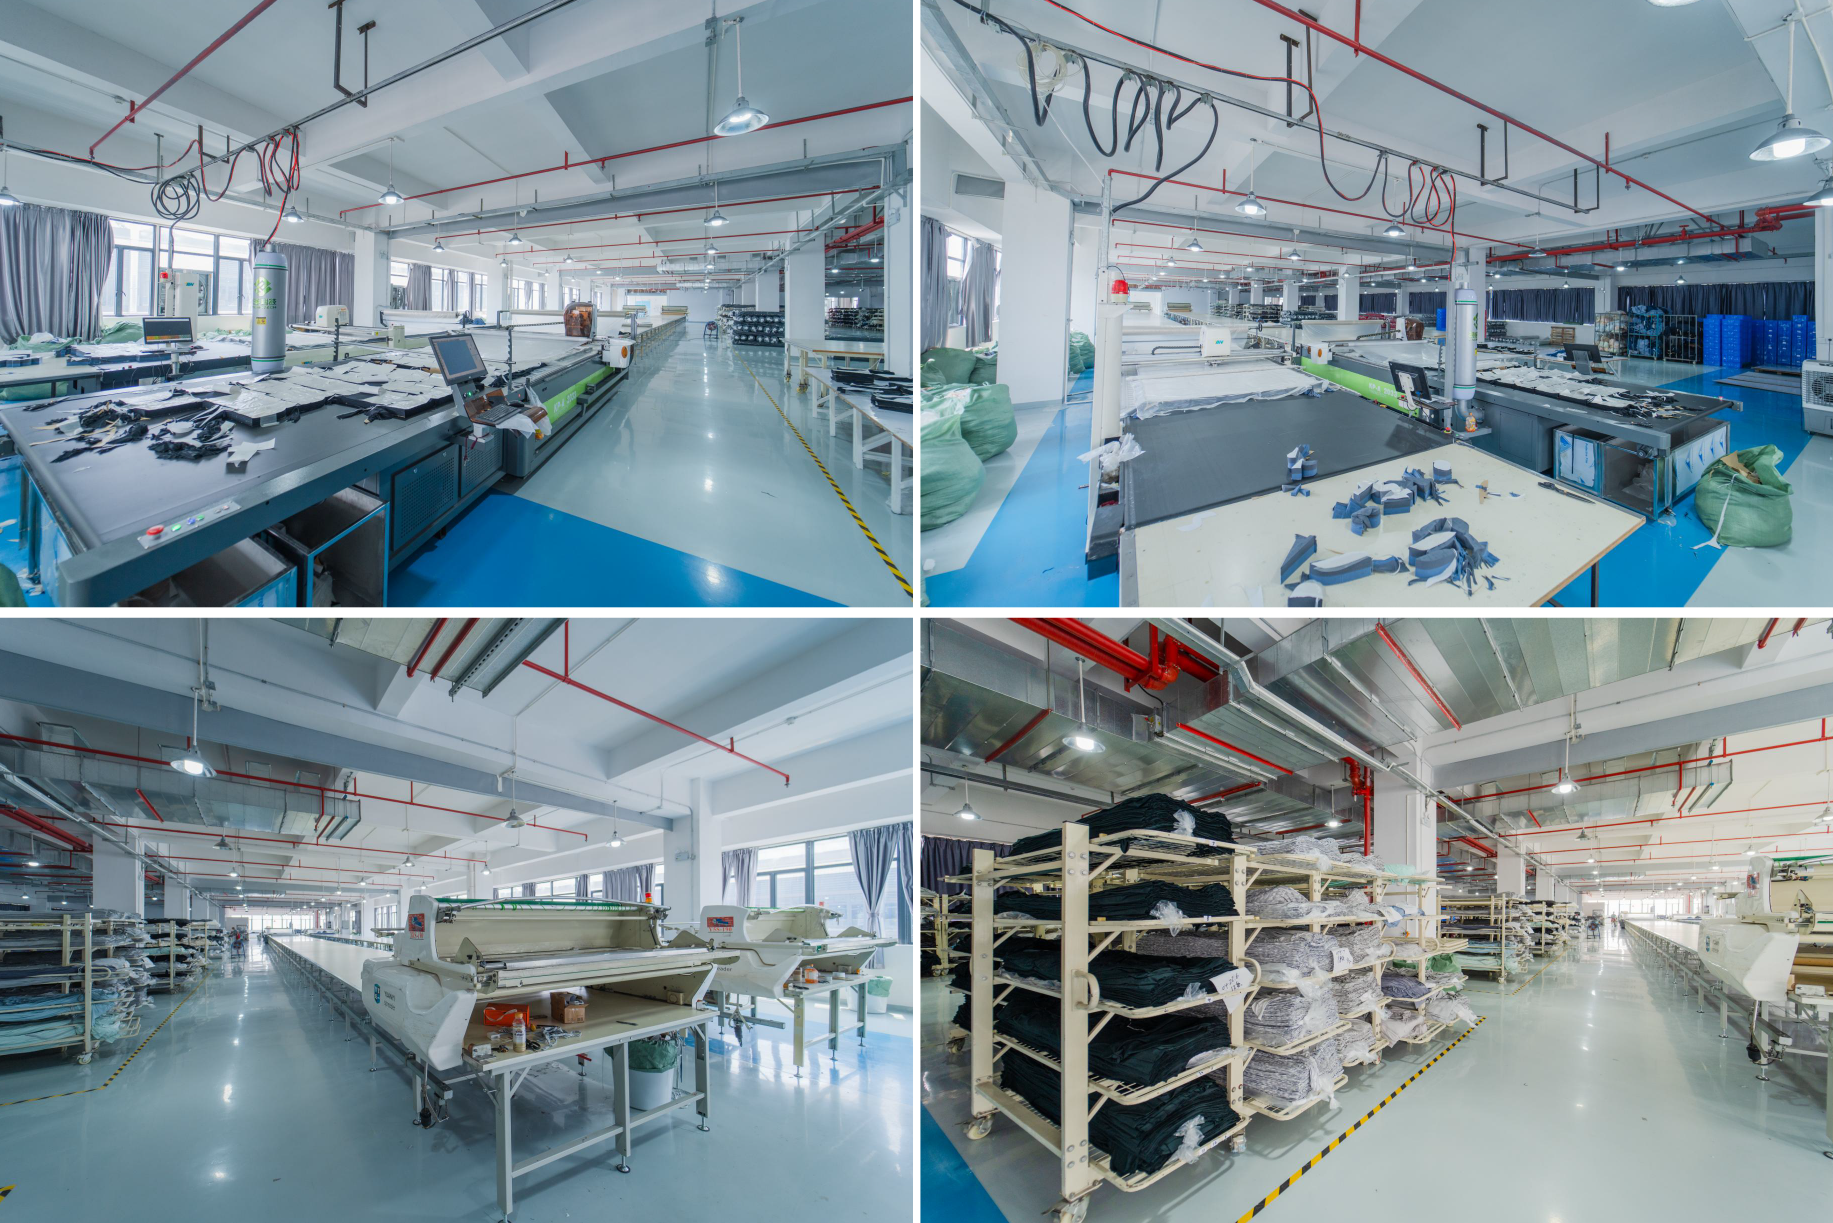
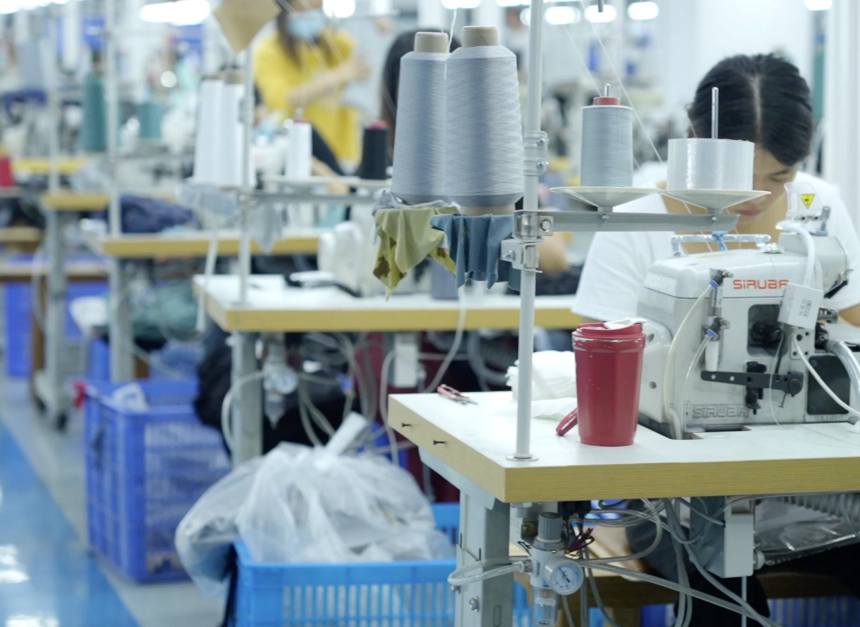
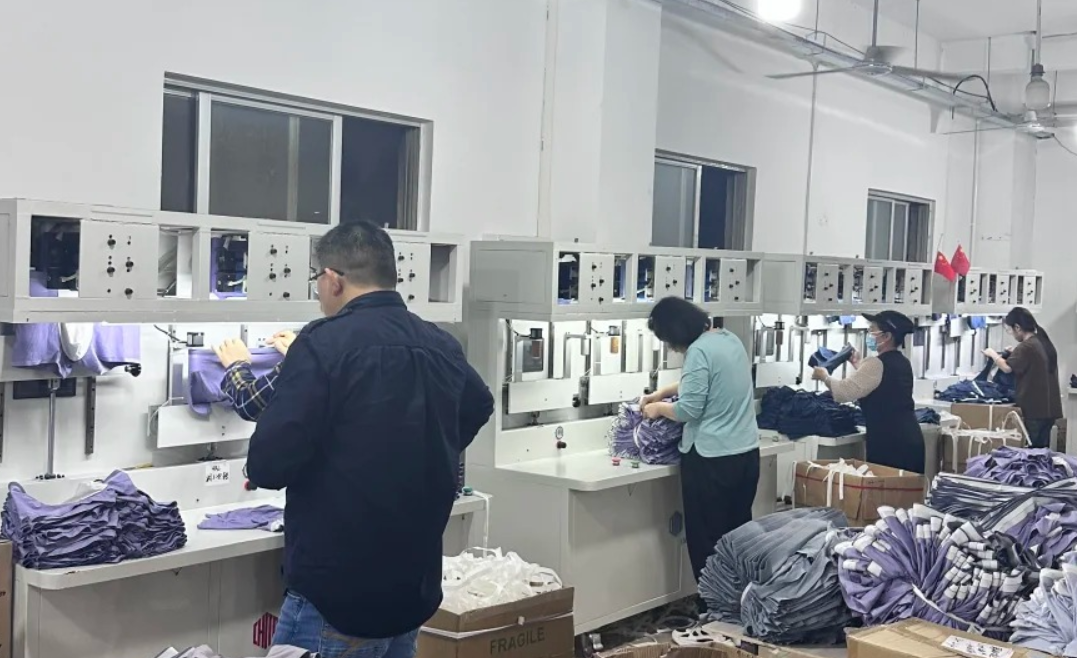
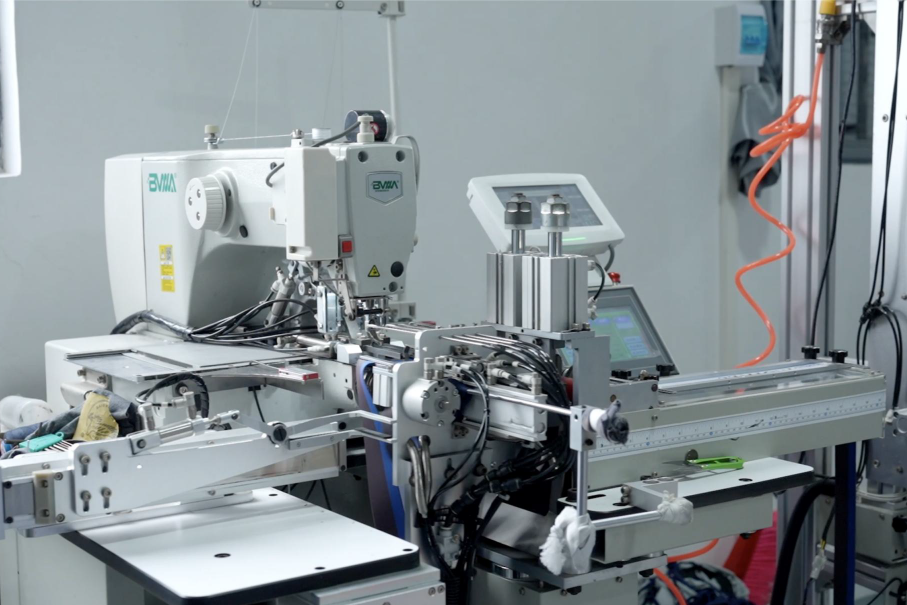
Efficiency meets precision on our production floors. Operated by over 180 textile specialists, our facility features 8 highly optimized, modern lean production lines. With a stable monthly output of 400,000 pieces and an annual capacity reaching 5 million garments, we effortlessly accommodate high-volume retail orders and seasonal inventory spikes. Our standardized 5S factory management ensures a fluid, responsive workflow, guaranteeing an agile lead time and seamless scalability for your brand's growth.
Strict End-to-End QC & 100% Metal Detection Guarantee
We implement a rigorous, uncompromising quality control system across the entire product lifecycle to protect your brand from retail returns. Our quality assurance protocol starts with strict incoming raw fabric audits and continues with meticulous in-line spot checks. Before boxing, every single garment undergoes a 100% comprehensive manual inspection for stitching integrity and dimensional accuracy. Finally, to ensure absolute consumer safety, 100% of export-ready shipments pass through advanced needle-detection machinery to guarantee a completely zero-metal, defect-free deliverable.
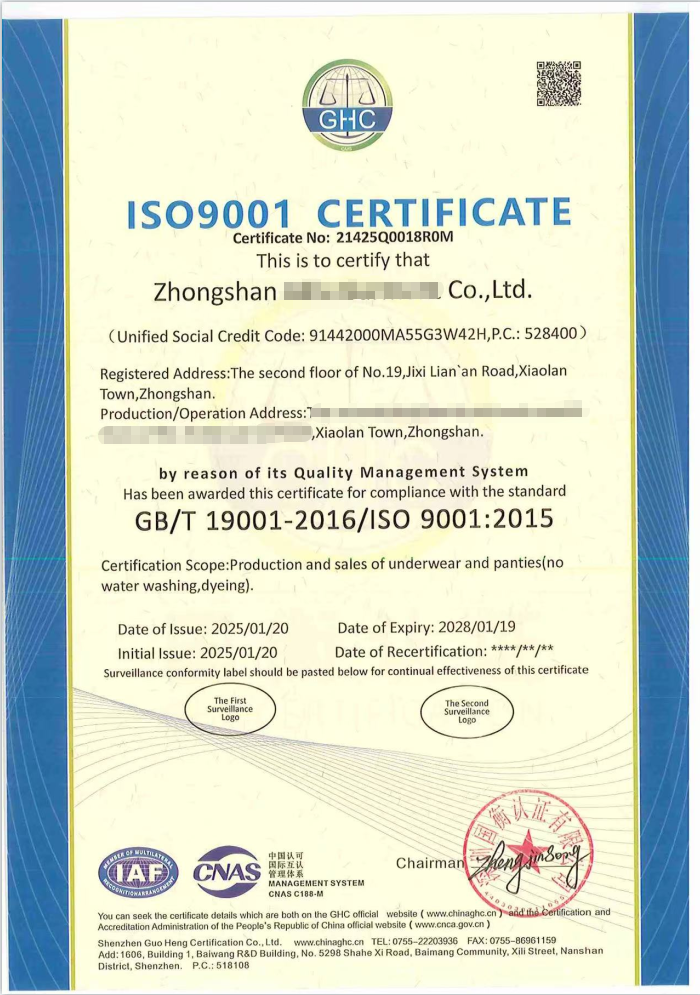
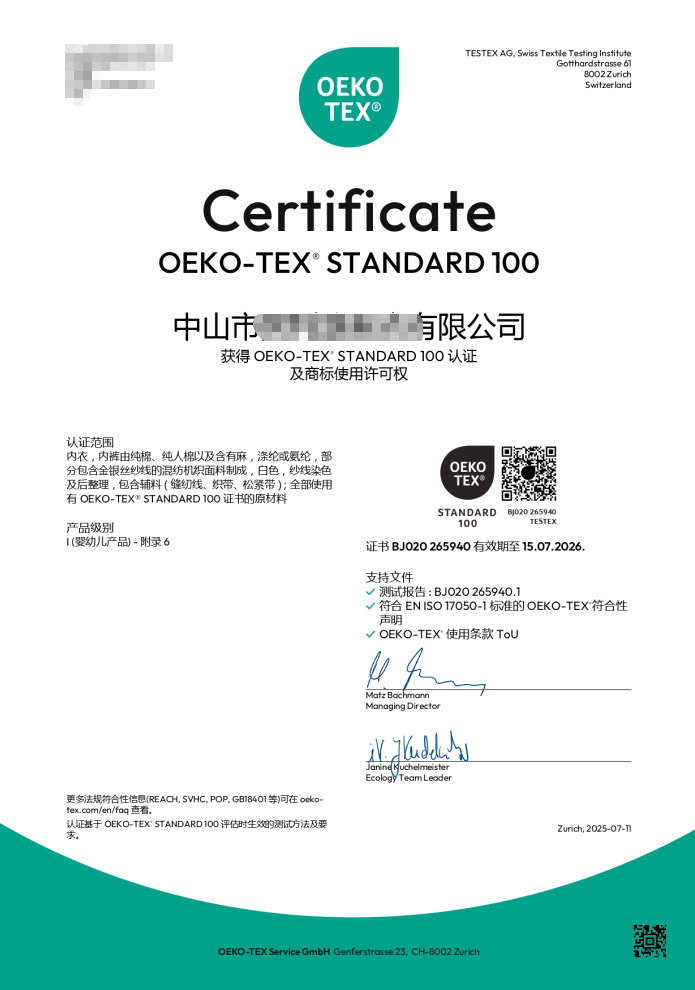
Certified Quality Management and Certified Product Safety
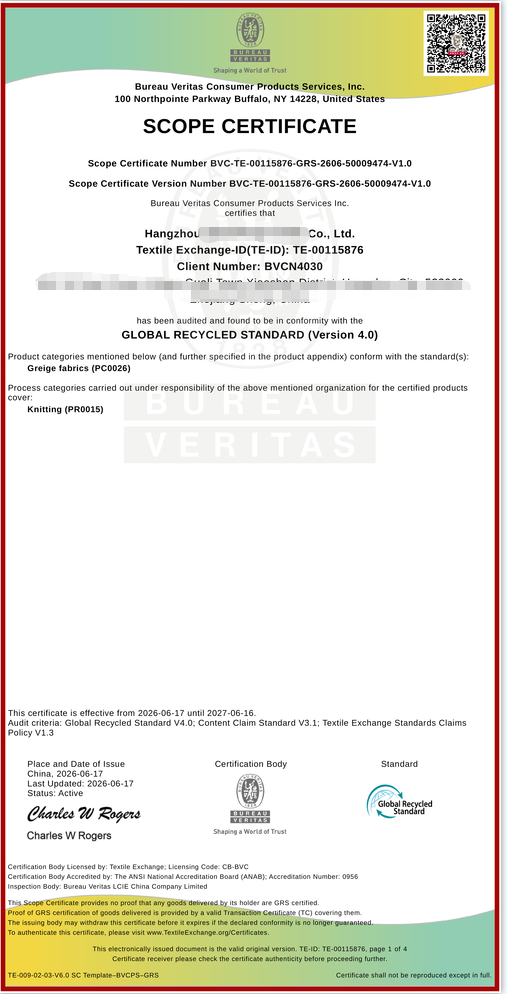
Your global compliance and peace of mind are built into every stage of our business. Our facility rigorously operates under the internationally recognized ISO 9001 quality management system, ensuring standardized, traceable, and continuous improvement across all production workflows. Furthermore, our products carry the prestigious OEKO-TEX Standard 100 ecological certification, guaranteeing that every fabric blend, dye, and waistband we use is entirely free from harmful substances and perfectly safe for sensitive skin. We are also GRS (Global Recycled Standard) certified, verifying our recycled-material supply chain and responsible production practices. Together, these credentials deliver verified compliance and uncompromised safety that meet the strict entry requirements of global retail markets.
Experienced Specialists Driving Retail Innovation
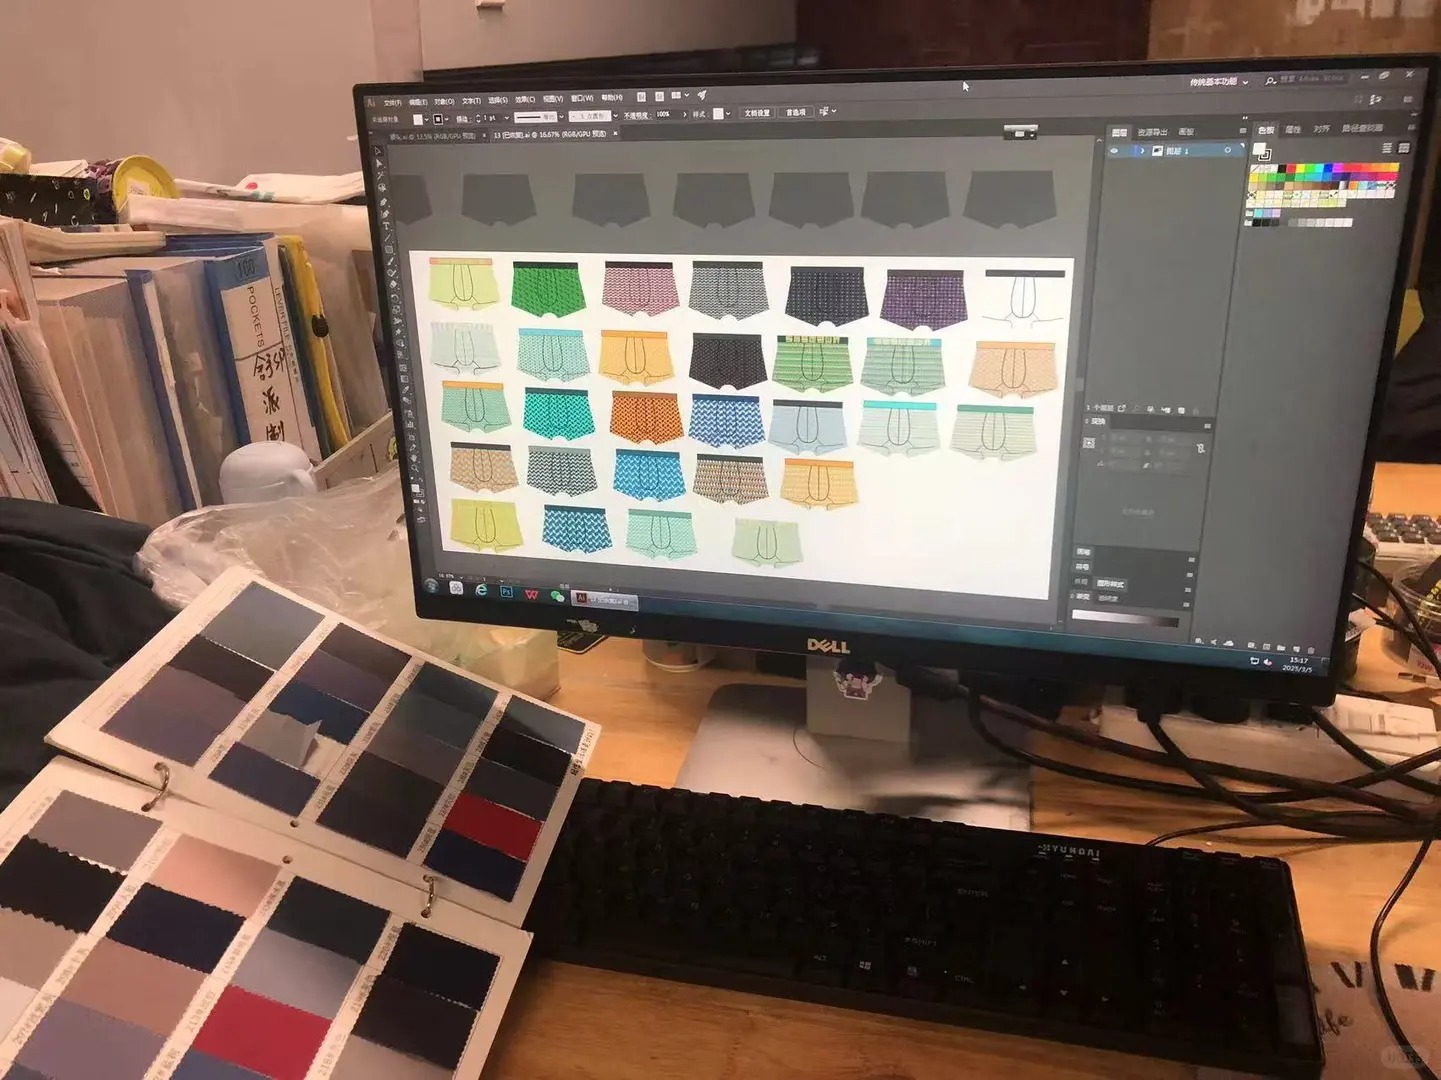
Behind our manufacturing power is a team of dedicated industry professionals. From experienced sample master craftsmen and precise technical pattern designers to our highly responsive, multi-lingual international trade division, we bridge the gap between concept and delivery seamlessly. Our team excels at understanding intricate overseas tech packs, offering professional optimization for fit and material choices, and providing clear, proactive communication throughout your entire manufacturing journey.
Exporting Excellence to North American and European Markets
We understand the high market entry barriers, strict labeling rules, and fast fashion cycles of western markets. The vast majority of our products are manufactured directly for premium brands, major retailers, and online private labels across North America and Europe. Having shipped millions of products overseas, we are fully versed in international shipping standards, custom clearance compliance, and major distribution hub requirements, making international sourcing frictionless for your brand.

Sustainable Manufacturing for Eco-Conscious Brands
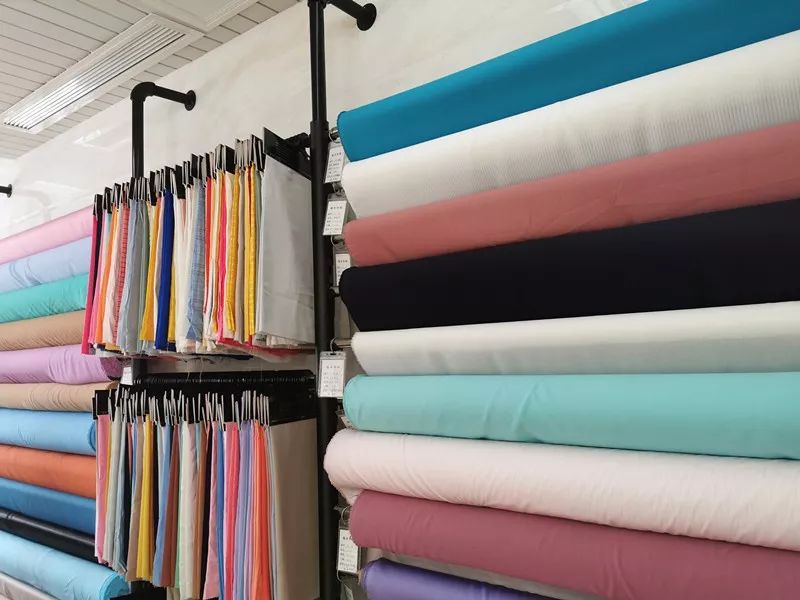
As part of our long-term vision, we are deeply committed to reducing the environmental footprint of fashion manufacturing. By utilizing OEKO-TEX certified low-impact non-toxic dyes and prioritizing sustainable fibers like Bamboo, Modal, and GRS-certified recycled polyesters, we help brands appeal to the modern eco-conscious consumer. Our factory constantly strives to optimize energy use and reduce textile waste, proving that high-volume manufacturing and ecological responsibility can go hand in hand.
Start Your Custom Underwear Project
Partner with a vertically integrated manufacturer committed to quality, scale, and your brand's growth.